The particular 3D printing method you use to fabricate an object plays a role in determining quality, and just as important is the design of the object to begin with. While a computer-controlled machine largely automates the printing process, it still requires effective implementation of DfAM (Design for Additive Manufacturing) guidelines to ensure efficient fabrication. Among the most important guidelines is minimizing material usage. This does not suggest that you should skimp on materials. Rather, an efficient design crafted with DfAM in mind prevents you from spending too much money on materials you actually don’t need. A good design can be fabricated using a minimum amount of materials, while still meeting all the necessary part requirements.
For businesses that need help applying DfAM principles to their designs, Cad Crowd connects you with experienced CAD designers, 3D modelers, and product development professionals who can optimize designs for additive manufacturing. By refining the design before it reaches the printer, businesses can reduce unnecessary material use, simplify production, and create parts better suited to efficient 3D printing.
RELATED: 3D Printing Technologies for Modeling and Prototyping
🚀 Table of contents
Another hallmark is simplification. In this case, simplification is not about making an object as rudimentary as possible. It has more to do with eliminating non-essentials while focusing on core features and functionality. This also directly affects material usage, as you won’t need as much as you otherwise would if you were to fabricate less-important frills. For instance, you want to 3D print a traditional pagoda lantern; it’s going to have a decorative chimney with a certain geometric pattern, but do you really need to put a gargoyle on top? A simple design saves on materials, prints faster, and therefore costs less.
And size really does matter in 3D printing. A large object takes longer to print and uses more material. Design complexity is, of course, a relevant consideration. A large yet simple hollow cube might be faster and cheaper to print than, say, a small yet highly detailed action figure. But assuming an object has no additional advantages from being bigger, why bother making it big at all? DfAM, when executed properly at least, does nothing but good things to the printed object. Think of it as a set of suggestions, with which you strive to build an effective design that’s structurally sound, functional as intended, and aesthetically pleasing while maintaining cost efficiency.
The printing methods
Before you can start optimizing anything, you must first consider the specific 3D printing service methods to use. There are a few, including FDM (Fused Deposition Modeling), SLA (Stereolithography), SLS (Selective Laser Sintering), MJF (Multi Jet Fusion), PolyJet, DMLS (Direct Metal Laser Sintering), and Electron Beam Melting (EBM). Some are pretty commonplace these days thanks to competitive pricing to the point where you can call them “consumer-grade”, while others remain solely used for industrial applications.’
RELATED: What Is 3D Printing? A Beginner’s Guide
The discussion today focuses on the optimization guidelines for three of the most popular 3D printing methods across both categories: FDM and SLA (consumer-grade) and SLS (industrial). We’re not going to get into the details of every single optimization method in existence, but just the very basics to get you started with additive manufacturing for general purposes.
FDM
Also known as FFF (Fused Filament Fabrication), a 3D printer using this method does so by extruding melted thermoplastic through a nozzle and stacking the material layer by layer until it forms the desired shape. Once the extruder finishes with one layer in the X and Y axes (horizontal orientation), it moves up by a small distance to deposit more material on top of the previous layer. The extruder keeps repeating the sequence until the build is complete.
Desktop FDM is relatively simple to operate and affordable, making it one of the most widely used 3D printer types among home users. The method works with a wide variety of materials, from common thermoplastics (PLA, PETG, and ABS) to exotic ones such as carbon fiber plastic and metal-infused filaments. As it turns out, being user-friendly and inexpensive doesn’t mean it can’t fabricate high-quality objects. But it has limitations, so it’s best to stick to DfAM practices to get the most out of your FDM printer.
RELATED: Comprehensive Guide to SLS 3D Printing Services for Companies
Feature size and wall thickness
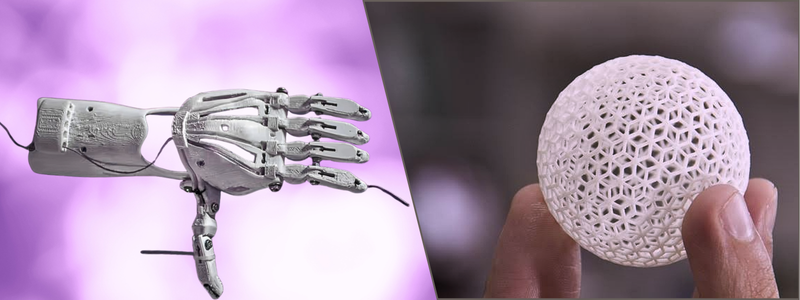
First things first, the minimum feature size in FDM is entirely dependent on the printer’s nozzle size. Many slicers (the programs that convert CAD files into commands 3D printers can read and execute; not identical to the G-Code used for CNC machining services, but not entirely different either) set the feature size to 120% of the nozzle diameter by default. Still, you can always configure it to 100% for simplicity reasons. For the vast majority of users out there, there’s no need to ever look at how this G-code works. If you use a Slicer program, much of the conversion happens automatically. An FDM 3D printer is sophisticated and all, but still essentially a printer. You don’t have to understand how a printer communicates with a computer to use both.
With that in mind, wall thickness is best set at an integer multiple of the printer’s extrusion width. For instance, if the nozzle extrudes the filament at the width of 0.4 mm, the wall thickness (for the object to be fabricated) should be 0.8 mm, 1.2 mm, 1.6 mm, and so forth. For general-purpose 3D printing, as opposed to the fabrication of exquisitely intricate objects with complex geometry and fine details, the recommendations for wall thickness are as follows:
| Feature | Wall Thickness | Wall Thickness |
| Feature | Minimum | Recommended |
| Vertically oriented walls | 0.8 mm | 1.2 mm |
| Horizontal surfaces (ceiling, floors, roof) | 0.8 mm | 1.0 mm |
| Free-standing, unsupported vertical walls | 1.0 mm | 1.5 mm |
| Load-bearing walls and structural elements | 1.5 mm | 2.0 mm |
Most FDM printers are fitted with the 0.4 mm nozzle as standard. A minimum wall thickness of 0.8 mm means the nozzle has to extrude two identical perimeter lines for each wall. In the event you decide to use a nozzle size of 0.6 mm or 1.5 mm (any non-integer nozzle size), the extrusion may create unwanted gaps between perimeter lines or, worse, skip an entire section. Having said that, a minimum of 0.8 mm isn’t always true because most, if not all, FDM 3D printers have a removable nozzle so that you can switch to a smaller or bigger extrusion width for different use cases.
RELATED: Why Additive Manufacturing is the Future of CAD and 3D Modeling Services for Engineering Firms
Overhangs
FDM deposits material onto the print bed below the extruder. Features that overhang or extend into the air without adequate support may fail or droop. As a rule of thumb, a 45-degree overhang is the maximum a feature can hold its own weight without risking unwanted deformation. Beyond that, support is almost always needed. Bridges wider than 20 mm also require support.
Anisotropy
Parts are anisotropic when fabricated using the FDM method. Because a part is formed one horizontal layer at a time, the tensile strength in the XY plane is inherently better than the Z axis (vertical orientation). Even when parts are printed with 100% infill rate (solid rather than hollow), air gaps between the layers are unavoidable. Solid parts rarely happen unless you’re printing structures or features designed to handle real loads. Anisotropic layers are inevitable issues, but there are mitigations. For instance, if the part is supposed to withstand tensile loads, make sure it’s printed in an orientation that runs parallel to the force. A pA perpendicular load (running along the Z-axis) increases the risk of delamination or layer separation. And for bending loads, orient the parts so that the highest stress runs along the bend of a continuous shell in the outermost layer (think of how you would normally bend a stack of plywood).
RELATED: How 3D Printing is Changing Product Design and Manufacturing
Holes and threads
One limitation of FDM printing is that the nozzle can’t trace a circular path precisely, leading to inaccurate hole diameters. You can compensate for the issue by adding (in the design) an extra 0.2 – 0.4 mm to its actual diameter.
| Hole Orientation | Diameter | Diameter | Notes |
| Hole Orientation | Minimum | Recommended | Notes |
| Vertical | 1.0 mm | 2.0 mm | Vertical holes can be printed well with good accuracy. If you have to use vertical pins, however, make sure it’s at least 3.0 mm in diameter otherwise it can be too fragile. |
| Horizontal | 2.0 mm | The top section of every horizontal hole is an overhang. Use tear drop shape (when possible) to mitigate the issue. | Support for the top section of the hole might be necessary. Or you can use lower layer height, which increases overall print time. |
As for threads, it’s recommended that you print the hole undersized and then drill it out to make up for the difference after printing. For example, a threaded hole is supposed to be 3.0 mm in diameter. Instead of printing to that exact dimension, you fabricate the part with a 0.1 mm-diameter hole and then remove the remaining 0.2 mm with a drill bit. Printed threads work, but they won’t provide as reliable connections as heat-set brass inserts, which essentially provide the strength of metal in plastic parts. The inserts are widely used in product prototyping.
Tolerances
While FDM is accurate for most basic shapes, it’s more of a practical fabrication method rather than a precision technology. The general tolerance for features smaller than 100 mm is 0.3 mm (or 3% of the nominal size), which isn’t exactly bad, but it isn’t excellent either. The larger the part, the more thermal stress it has to withstand. Materials like nylon and ABS are especially susceptible to warping from exposure to heat. At the same time, they also suffer from shrinkage as temperature drops quickly after printing.
SLA
If the part requires tighter tolerances and better surface finish, SLA can be the printing method of choice. SLA is in fact the oldest form of 3D printing services based on vat photopolymerization. It prints by emitting controlled UV light into a vat of resin to cure and solidify the material selectively, one layer at a time. Layer height in SLA can range from 25 to 50 microns, enabling fabrication of a surface finish nearly as smooth as injection molding. Despite using only “resin” as the material, this type of plastic comes in a wide variety of options, including biocompatible, heat-resistant, transparent, flexible, rigid, and so forth. However, like FDM, even SLA has limitations.
RELATED: How 3D Printing for Rapid Manufacturing Is Pushing Boundaries at Product Design Services Firms
Wall thickness
Upside-down or inverted stereolithography is the most common system. The build platform, from which the UV light is emitted, is positioned above the liquid resin. To do the printing, the platform lowers into the tank, leaving only a thin layer of resin between the components. At the end of the process, the printed part/object is hanging from the platform with a substantial support structure.
While it’s possible to print walls without a support structure, it may break off, especially if it’s too thin. Unsupported walls should be at least 0.6 mm thick to minimize the risk of warping, but you can get away with 0.4 mm thickness with support. Keep in mind that thin walls cool quicker than their thicker counterparts. Maintain uniform thickness throughout the build to prevent defects.
Tolerances
Although the printing itself is accurate, shrinkage during curing must be accounted for. Also, there needs to be adequate clearance between mating parts to prevent them from fusing when printing. A minimum clearance of 0.5 mm is required between parts.
RELATED: Why Businesses Should Consider 3D Printing Services and Prototyping for Product Design
Holes or hollow parts
The inverted build platform isn’t exactly designed for hollow sections or concave shape features because they can trap uncured resin, leading to internal pressure imbalances and cracks. As a workaround, make sure to include a drainage hole in every fully enclosed cavity (if the part design allows) to let excess resin escape.
The walls of a hollow section must each be at least 2 mm thick. Even if there’s an amount of liquid resin trapped inside (before it escapes through the drainage hole), the structure should be rigid enough not to crack or deform. A single drainage hole must be 4.0 mm in diameter or larger. If you plan to use multiple escape holes, a diameter of 2.0 mm each should be sufficient. Multiple escape holes are recommended for hollow sections measuring 50 x 50 x 50 mm (H x W x D) or larger.
Post-curing warping on thin parts
Since the 3D printing design process relies on ultraviolet light and heat to harden the resin, post-curing is an essential step in every fabrication process. Heat and light solidify the material during printing. In post-curing, they harden the part further but also cause shrinkage. If curing doesn’t occur at the same rate throughout the build, thin features may warp. Placing the entire printed object directly on the turntable (of the post-curing machine) can help minimize the risk.
RELATED: 6 Ways You Can Use 3D Printing Services to Create a New Prototype Design
SLA prints accurate objects with a high-quality surface finish when given proper post-processing. That said, SLA-printed objects tend to fade and become brittle with prolonged exposure to light. Thermoplastic materials used in the FDM method are not light-sensitive.
SLS
“Selective Laser Sintering” is a pretty self-explanatory term in the 3D printing context. SLS utilizes high-power lasers to selectively fuse or sinter tiny particles or powder of thermoplastics (most commonly nylons and TPU) to form an object. Unlike FDM and SLA, you don’t need to build a dedicated support structure with SLS because the unsintered particles surrounding the printed parts provide the same (perhaps even better) function. Such an advantage unlocks greater design freedom, allowing you to build complex shapes with interlocking parts, organic geometry, and internal channels without risk of deformation and warping. But then again, it’s not without limitations.
RELATED: 3D Printing Services, Cost and Rates for Companies and Firms
Feature size
Details and features that are too small in size may not sinter completely. The minimum feature size in SLS is 1.0 mm, which isn’t that great for intricate geometry but more than adequate for most practical purposes. It’s possible to print a smaller-sized feature, but there’s always a risk of the feature ending up missing from the finished part. If you have to include pins, posts, or any protruding cylindrical feature, make sure they have a 1.5 mm diameter each to prevent breakage.
Escape holes
You only need to design an escape hole if the part contains a completely enclosed cavity, so that the unsintered particles can flow out with no meaningful restriction. A semi-enclosed hollow section shouldn’t be a problem. Even if some particles can’t escape on their own, light brushing or an air duster should handle the cleaning task just fine.
- If there needs to be an escape hole in the part, it should be at least 1.5 mm in diameter.
- An escape hole is ideally positioned at the bottom of an enclosed cavity, but this is not mandatory because you have to take the part out of the powder bed anyway for cleaning. As far as positioning is concerned, the more important consideration is functionality. The hole shouldn’t be positioned in a spot where it affects part function.
- For complex parts with internal channels and structures, connection points/mounting holes may serve a dual purpose as drainage openings as well, so long as the diameter is adequate.
One of the biggest limitations of SLS is sealed chambers. SLS can’t fabricate a fully enclosed cavity without trapping powdered materials inside. You can, of course, drill an escape hole after printing, although this might negatively affect the structural rigidity of the part.
RELATED: A Brief History of 3D Printing
Wall thickness
The minimum recommended wall thickness with SLS printing is 0.7 mm. To maintain an ideal strength-to-weight ratio, however, wall thickness is best set anywhere between 1.0 mm and 2.0 mm. But be careful because thicker isn’t always better. Beyond 8.0 mm, the materials can instead become too brittle from cooling stresses during the sintering process. As always, aim for consistent thickness throughout the build to prevent warping. Nylons are by far the most popular materials for SLS because the finished part is “nearly” isotropic. Features in the horizontal plane (X and Y axes) are still stronger than those along the Z axis, but not by much. For most practical purposes, the structure across the X, Y, and Z planes is structurally sound and genuinely functional with almost no weak bond between layers, even under load.
Clearances for mating parts
SLS makes it much easier to fabricate multiple parts in a single printing session. Assuming the parts are all part of an assembly, it’s crucial to take into account the clearances between mating parts for the right fit. The dimensional tolerances in SLS are given at 0.3 mm, which should come into play when designing an assembly. Sliding fit typically has a gap of anywhere from 0.2 mm to 0.5 mm between the parts, whereas snug fit must be designed with 0.1 mm – 0.2 mm interference (as opposed to gap) in mind.
RELATED: How 3D Modeling is Beneficial in Product Manufacturing & New Product Development Services
What to choose
Every 3D printing technique has its own advantages and drawbacks, with different use cases for the fabricated parts as well. You choose a technique that best serves the purpose. Here is a simple comparison between FDM, SLA, and SLS for reference.
| 3D Printing Technique | Material | Surface finish quality | Structural strength | Details | Cost per part | Usage |
| FDM | Thermoplastic filament | Low to Medium | Low to medium | Low to medium | Lowest | PoC prototypes, brackets, toys, simple non-aesthetic structures |
| SLA | Photopolymer resin | Very high | Low to medium | Very high | Low to medium | Looks-like prototypes, visual models, simple medical devices, jewelry |
| SLS | Nylons and TPU powder | High | High | Medium to high | Medium to high | Functional prototypes, low-volume production units |
Closing thoughts
3D printing, whether FDM, SLA, or SLS, makes for an excellent rapid prototyping method in addition to CNC machining. Both methods are accurate, but there are some glaring differences. 3D printing is still heavily associated with plastic materials despite its ability to work with metal-infused filaments, whereas CNC machining remains the preferable method when working with metal and wood, although it too can process plastic. Another important distinction is that 3D printing needs no draft, which is otherwise a crucial feature in CNC machining.
But then again, no matter which technique you choose, it’s only as good as the printable file fed into the machine. The most advanced 3D printer won’t be able to fabricate high-quality parts if the printable file is of subpar quality in terms of details and accuracy. Cad Crowd is where you’ll discover the most talented CAD and additive manufacturing professionals, specializing in part designs for both prototyping and end-user purposes. Every model is optimized for the printing technique of your preference, delivered in watertight STL or 3MF format along with the parametric source.
RELATED: How 3D Printing & CAD Services Will Revolutionize New Product Development at Your Company
How Cad Crowd can help
Cad Crowd connects businesses with experienced CAD designers, 3D modelers, and additive manufacturing professionals who can help optimize product designs for different 3D printing methods. Whether you are working with FDM, SLA, or SLS, our professionals can help refine features such as wall thickness, tolerances, clearances, overhangs, holes, and overall part geometry. They can also prepare print-ready models that are better suited for efficient fabrication and rapid prototyping. Contact Cad Crowd today for a free quote and find the right CAD and additive manufacturing expertise for your 3D printing project.